Tool and process review
Review draft, parting line, slides, ejector locations, gate strategy, overflow, thermal control and expected tool life before release.
Manufacture repeat metal parts through one coordinated route covering tooling review, die casting, trimming, CNC secondary machining, surface finishing and dimensional inspection.
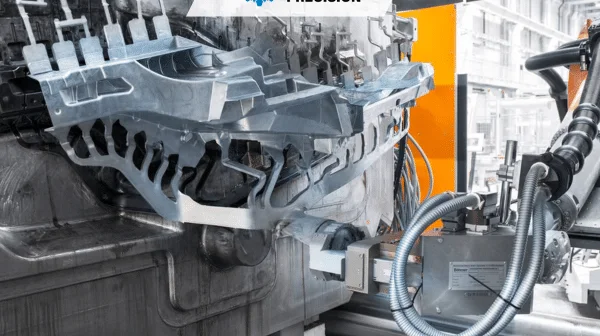
Die casting is most effective when alloy behavior, wall transitions, gate and overflow strategy, ejection, machining allowances and finishing requirements are reviewed as one production system.
Review draft, parting line, slides, ejector locations, gate strategy, overflow, thermal control and expected tool life before release.
Route repeat components around alloy, geometry, wall thickness, projected area, quantity and required mechanical or cosmetic performance.
Add controlled bores, threads, sealing faces, datum features, deburring, blasting, coating, plating or painting after casting.
Each stage confirms the next decision so casting, secondary machining and finishing remain tied to the approved drawing.
Confirm CAD, drawing, alloy, volume, finish, critical features and required records.
Review fill, venting, ejection, machining stock, cosmetic zones and tool architecture.
Build the tool, produce initial samples and document open dimensional or cosmetic issues.
Trim, machine, deburr and finish the casting according to the released route.
Verify agreed characteristics and records before packaging and shipment.
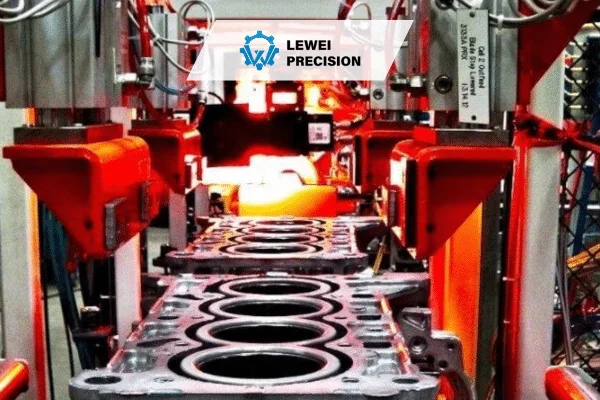
Stable die-cast parts depend on consistent wall sections, practical draft, controlled transitions and realistic expectations for cast versus machined features.
Availability and suitability are confirmed during project review. Exact alloy, temper, coating standard, color and cosmetic criteria belong in the RFQ.
Common for housings, brackets, covers and equipment components requiring a balance of weight, strength and finish options.
Suitable for smaller components, detailed geometry and applications that benefit from good castability and finishing response.
Options may include as-cast, blasting, polishing, conversion coating, plating, powder coating and painting, subject to alloy and specification.
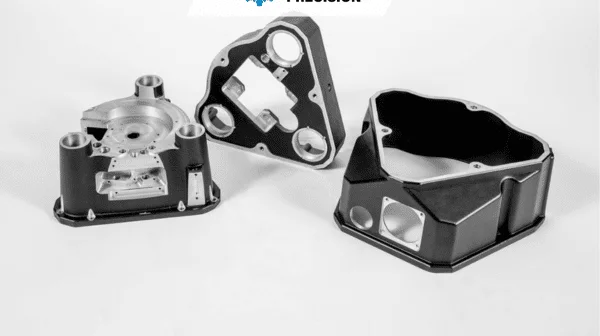
Acceptance may involve cast dimensions, machined datums, threads, sealing surfaces, coating appearance and assembly interfaces. Define critical characteristics and documentation requirements before tool release.
Die casting is typically considered for repeat quantities where tooling investment can be distributed across production and the geometry benefits from fast cycle times, integrated features and controlled secondary operations.
Yes. Critical bores, threads, sealing faces and datum features are often machined after casting. Machining stock, fixturing and datum strategy should be included in the process plan.
Send a 3D model, controlled 2D drawing, alloy, quantity, finish, cosmetic zones, inspection requirements and expected repeat demand.
Engineering will review the geometry, alloy, tooling approach, secondary operations, finish and inspection scope before quotation.